Blog de lvobo
Hogar

Blog

Blog

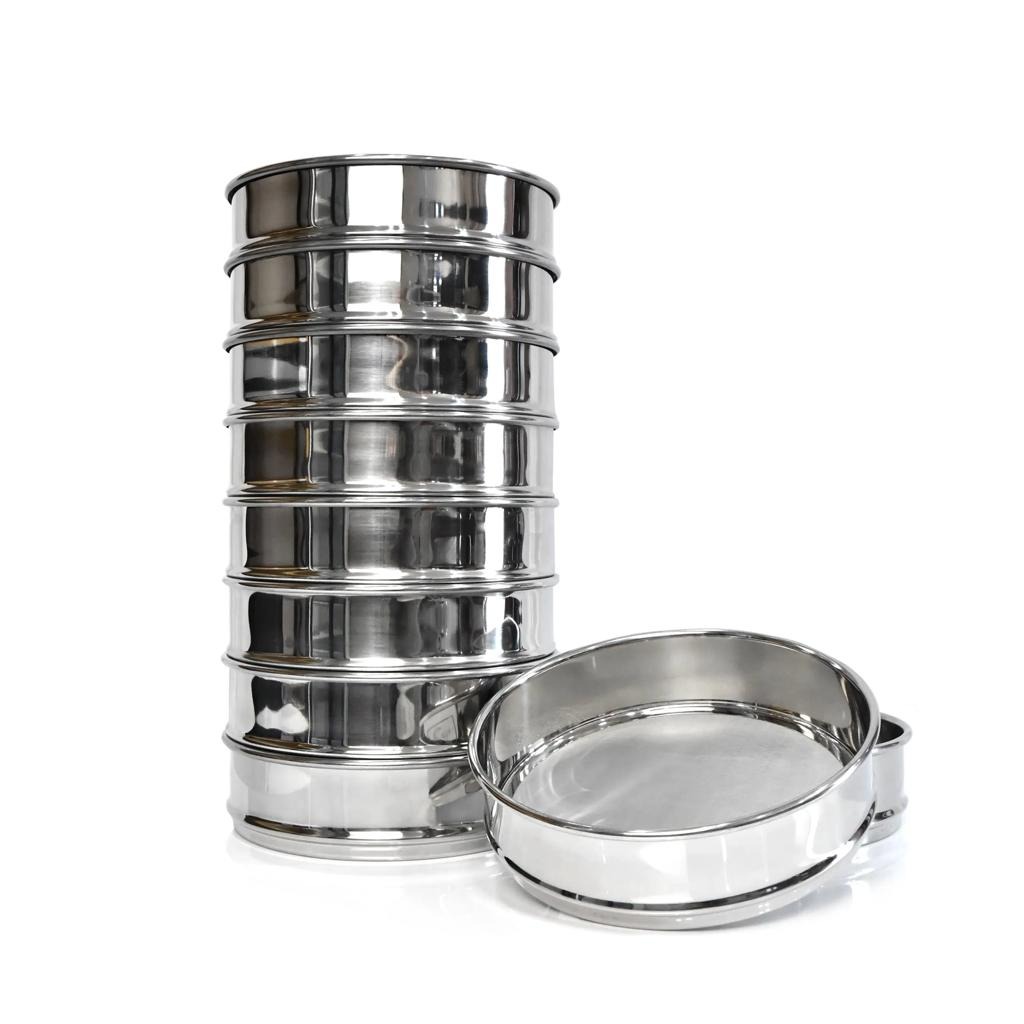
  • Electromagnetic Sieve Shakers in Laboratory Particle Size Analysis: Principles and Method Considerations
    Electromagnetic Sieve Shakers in Laboratory Particle Size Analysis: Principles and Method Considerations
    Oct 30, 2026
    Abstract Sieve analysis is a commonly used method for determining the particle size distribution of powders and granular materials. The reliability of the results depends on several factors, including sample characteristics, sieve aperture selection, sample loading, sieving motion, and test conditions. Electromagnetic sieve shakers provide a mechanical approach to laboratory particle separation through controlled electromagnetic excitation. This article examines the basic principles of sieve analysis, the factors affecting measurement results, and the considerations involved in selecting an electromagnetic sieve shaker for laboratory applications. 1. Principles of Laboratory Sieve Analysis Sieve analysis separates particles according to their ability to pass through defined sieve apertures. A series of test sieves with progressively smaller openings is commonly arranged in a stack, allowing a sample to be divided into several particle size fractions. During the test, particles interact with the sieve openings through movement, contact, and changes in orientation. Particles that pass through an aperture are collected in the next sieve or receiving pan, while larger particles remain on the corresponding sieve. The resulting distribution is generally expressed as the mass percentage retained on each sieve or passing through a specified aperture. It is important to distinguish sieve size from an absolute geometric particle diameter. For irregularly shaped particles, the probability of passing through an aperture can depend on particle orientation as well as its dimensions. 2. Electromagnetic Excitation and Sieving Motion The motion applied to a sieve stack influences how particles are distributed across the sieve surface and how frequently they encounter the mesh openings. In vibratory sieving, particle movement can involve vertical displacement combined with lateral or circular motion. This produces a three-dimensional movement pattern in which particles are repeatedly lifted, redistributed, and brought into contact with the sieve surface. An electromagnetic sieve shaker uses electromagnetic excitation to generate the driving vibration. The vibration is transferred to the sieve assembly, where the resulting motion supports particle separation. Amplitude is one of the important parameters affecting sieve movement. Changes in amplitude influence the intensity of particle movement and should be considered together with sample properties and sieve loading. The appropriate operating conditions are material-dependent. A single setting should not be assumed suitable for all powders and particle size ranges. 3. Factors Affecting Sieve Analysis Results Sieve analysis is influenced by both the physical properties of the sample and the conditions under which the test is performed. 3.1 Sample Representativeness The test sample should represent the original material as closely as possible. Particle segregation may occur during storage, transportation, or handling, resulting in differences between the collected sample and the bulk material. Sample mixing and appropriate sample division are therefore important steps before testing. 3.2 Sample Quantity and Sieve Loading The amount of material placed on a sieve affects the distribution of particles across the mesh surface. Excessive loading can create a thick particle layer, reducing the available contact area between particles and sieve openings. Insufficient sample quantities, on the other hand, may not adequately represent the original material. Sample quantity should be considered in relation to particle size, material density, sieve diameter, and the required measurement procedure. 3.3 Particle Properties Several material characteristics can influence the sieving process: Particle size distribution Particle shape and aspect ratio Bulk density Moisture content Agglomeration tendency Electrostatic charging Fine powders and particles with strong interparticle attraction may form agglomerates or adhere to the sieve mesh. These conditions can affect particle passage and the resulting size distribution. 3.4 Sieve Aperture and Condition Sieve selection determines the particle size intervals obtained during analysis. The selected apertures should cover the expected particle size range and correspond to the required classification intervals. The physical condition of the sieve is also important. Blocked, damaged, or contaminated mesh openings can influence the separation process. Test sieves should therefore be inspected and cleaned using methods appropriate to their mesh construction. 3.5 Operating Conditions Vibration amplitude, sieving duration, sample loading, and the characteristics of the material can all influence the observed results. For comparative testing, the operating conditions should be documented and kept consistent. Changes in test conditions may produce differences in particle distribution even when the original material is unchanged. 4. General Procedure for Laboratory Sieve Analysis A typical laboratory sieve analysis involves the following stages: Step 1 — Sample Preparation Obtain a representative sample from the original material. Mix and divide the sample when necessary. Step 2 — Sieve Selection Select the sieve diameters and aperture sizes according to the expected particle size distribution and the required number of fractions. Step 3 — Initial Weighing Determine and record the initial sample mass using an appropriate balance. Step 4 — Sieve Assembly Arrange the test sieves in the selected sequence, with larger apertures above smaller apertures, and secure the sieve stack. Step 5 — Sieving Apply the selected sieving method and documented operating conditions. The sample moves across the sieve surfaces and is separated according to the corresponding apertures. Step 6 — Fraction Recovery Collect the material retained on each sieve and in the receiving pan separately. Step 7 — Weighing and Evaluation Determine the mass of each recovered fraction and calculate the corresponding mass percentages. Step 8 — Sieve Inspection Inspect and clean the test sieves before subsequent measurements. 5. Evaluation of Particle Size Distribution The results of sieve analysis are generally evaluated using the mass of material retained on individual sieves. The mass percentage retained on a particular sieve can be calculated as: Mass Percentage Retained (%) = (Mass of Fraction / Total Recovered Mass) × 100 The cumulative retained percentage is obtained by adding the retained percentages from the largest aperture down to the sieve being evaluated. The cumulative passing percentage can then be calculated as: Cumulative Passing (%) = 100 − Cumulative Retained (%) Results may be presented in a data table or particle size distribution curve. The mass balance between the initial sample and the recovered fractions should also be checked. Any material loss should be recorded because it may affect the interpretation of the results. 6. Considerations When Selecting an Electromagnetic Sieve Shaker The selection of laboratory sieving equipment should be based on the intended test method and the characteristics of the material. The following factors are generally considered: Selection Factor Technical Consideration Sample Characteristics Particle shape, density, moisture and agglomeration Particle Size Range Expected minimum and maximum particle sizes Sieve Diameter Available working area and sample loading Sieve Apertures Required particle size intervals Number of Fractions Number of sieve layers required Vibration Amplitude Suitable vibration intensity for the sample Sample Quantity Required mass for each test Test Conditions Repeatability and consistency of operating parameters The equipment configuration should be evaluated against the laboratory's actual testing requirements rather than selected solely by nominal machine capacity. 7. Electromagnetic Sieve Shaker: BO-300ESS Technical Example The LVOBO BO-300ESS is an electromagnetic sieve shaker developed for laboratory particle size analysis, powder classification, and sieve residue testing. Its operating system uses electromagnetic excitation to generate high-frequency reciprocating vibration and three-dimensional sieving motion. The main configuration includes: Parameter Specification Model BO-300ESS Excitation Method Electromagnetic Input Voltage AC 220V Input Power 1000 W Amplitude 0–3 mm, continuously adjustable Sieve Diameter 200 mm / 300 mm Available Mesh Range 8–2000 mesh, depending on configuration Sieve Layers 1–7 layers Approximate Sample Capacity 5–1000 g per batch Control Interface Touchscreen Recipe Management Multiple recipe storage and recall Main Unit Dimensions D420 × W380 × H295 mm, without sieve stack The actual sample capacity depends on material properties, particle size distribution, sieve aperture, and testing requirements. The available sieve configuration should also be confirmed according to the intended application. These specifications describe the equipment configuration. They do not replace the need to establish and validate suitable testing conditions for individual materials. 8. Conclusion Laboratory sieve analysis involves more than selecting a sieve shaker and a set of test sieves. Sample representativeness, particle characteristics, sieve aperture selection, sample loading, operating conditions, and data evaluation all contribute to the final particle size distribution. Electromagnetic excitation is one of the available approaches for generating vibratory motion in laboratory sieve analysis. Its application should be evaluated in relation to the material being tested and the requirements of the analytical procedure. A well-defined testing method, together with appropriate equipment configuration and consistent sample handling, provides the basis for meaningful particle size analysis and comparison between laboratory tests. Technical Note This article provides general technical information on laboratory sieve analysis. Specific testing procedures, operating conditions, and acceptance criteria should be established according to the material, applicable test method, and laboratory requirements.
    LEER MÁS
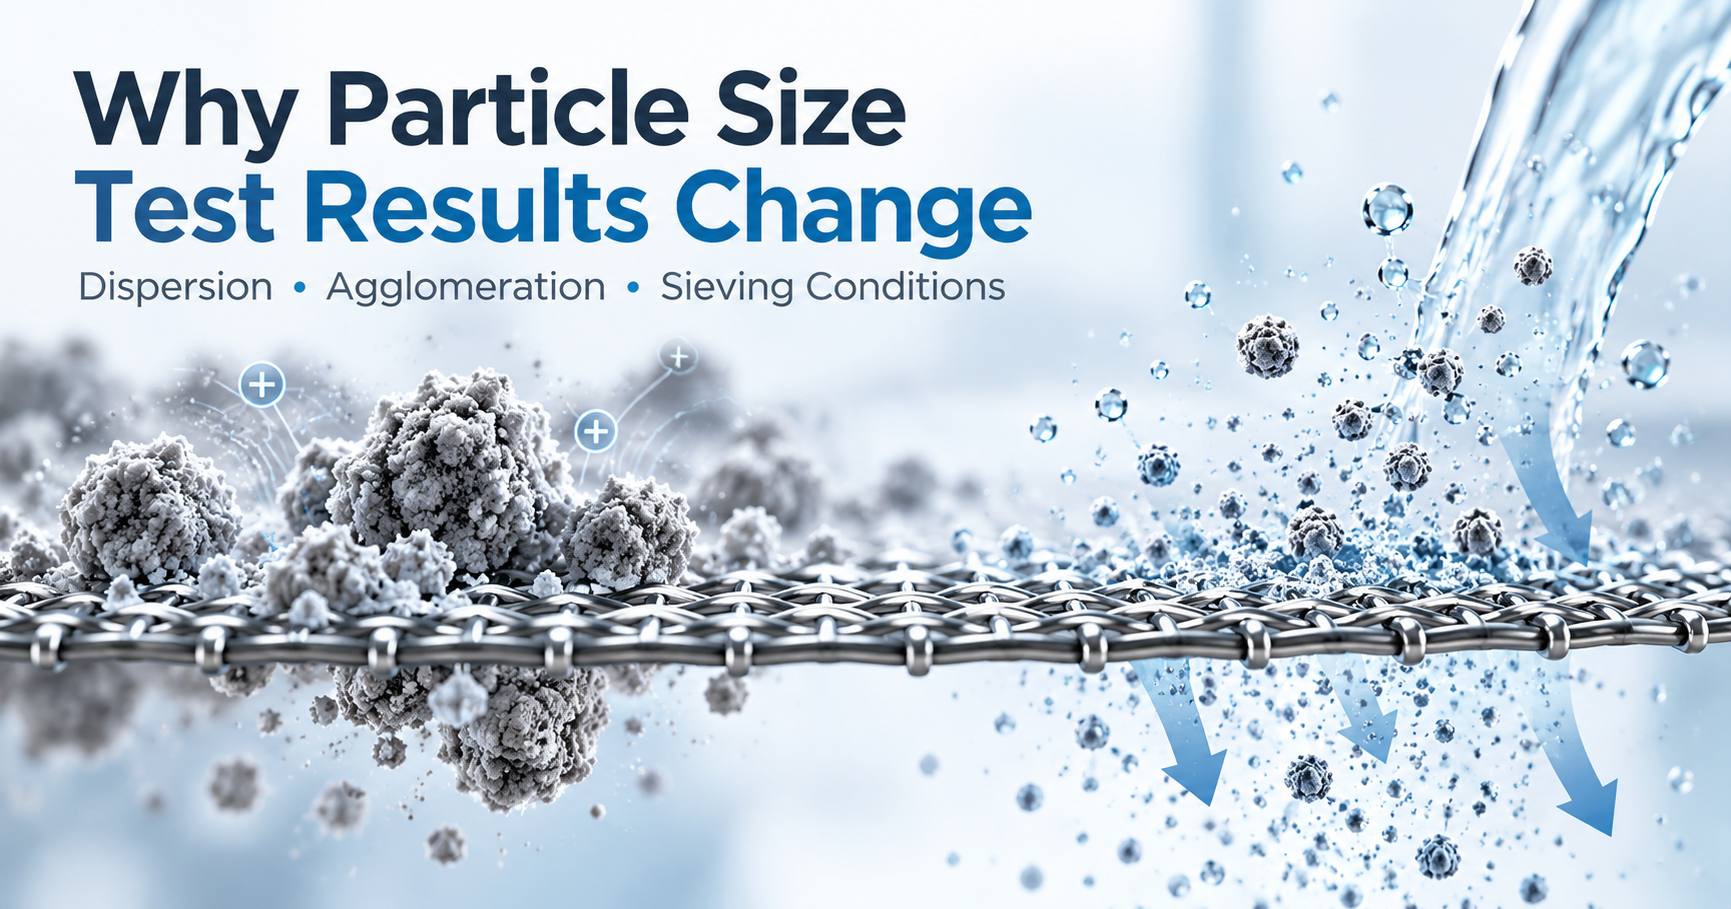
  • Why Particle Size Test Results Change: Dispersion, Agglomeration and Sieving Conditions
    Why Particle Size Test Results Change: Dispersion, Agglomeration and Sieving Conditions
    Oct 26, 2026
    Particle size is often treated as a fixed property of a powder. In practice, however, the reported result also depends on the physical state of the sample and the method used to measure it. A powder tested in an agglomerated dry state may behave differently after liquid dispersion. Fine particles affected by static electricity may remain on a test sieve even when their dimensions would otherwise allow them to pass. Changes in sample preparation, sieving time, dispersion conditions, or measurement principle can also affect the reported particle size distribution. This means that when two laboratories test the same material and obtain different results, neither laboratory has necessarily made an error. For QC and procurement engineers, the more useful question is not simply: “What is the particle size?” It is: “Under what sample condition and test method was that particle size measured?” Why Do Particle Size Test Results Change? Particle size results can change because the powder state and test conditions change. Agglomeration, dispersion, static electricity, wet or dry testing, sample preparation, test duration, and measurement principle can all affect the reported particle size distribution. Results should only be compared when the test method and sample conditions are controlled. When Agglomeration Makes Fine Powder Look Coarser Fine powders do not always behave as independent particles. Moisture, electrostatic attraction, surface forces, and handling conditions can cause smaller particles to associate with one another. When this happens, a test may respond to the agglomerate rather than to the individual particles inside it. In mechanical sieving, an agglomerate may remain above the sieve opening even though the individual particles would be small enough to pass. The retained fraction may therefore contain both genuinely oversized particles and clusters of smaller particles that have not been sufficiently dispersed. For supplier qualification, batch comparison, or incoming inspection, sample preparation and dispersion conditions should be controlled before numerical results are compared. When Dispersion Changes the Measured Distribution Dispersion can also change what the measurement system sees. A recent Malvern Panalytical application study used time-resolved laser diffraction to monitor spray-dried alumina granules during ultrasonic dispersion. As dispersion progressed, a coarser particle population decreased while a finer population became more pronounced. The important point is not the individual particle-size values. It is that the measured distribution changed as the physical state of the sample changed. Ultrasonic energy, liquid media, mixing conditions, and dispersion time may separate agglomerates or otherwise alter the particle population presented to the measurement system. This creates a practical laboratory question: At what point does dispersion reveal the particle state relevant to the application, and at what point does additional energy begin to alter that state? There is no universal answer. Different materials can respond differently to the same preparation procedure. For this reason, particle size methods should specify not only the instrument, but also the sample preparation and dispersion conditions. When Static Electricity Distorts Dry Sieving Dry sieve analysis introduces another important source of variation: electrostatic charge. Fine particles may adhere to the sieve mesh, sieve frame, container surfaces, or other particles. This can make an electrostatic problem look like a particle-size problem. If fine powder remains above the sieve, the immediate conclusion may be that those particles are larger than the sieve opening. But some particles may actually be small enough to pass and remain on the mesh because of static attraction or loose agglomeration. Increasing vibration does not necessarily eliminate the underlying electrostatic interaction. For laboratory sieve analysis, visible adhesion to the mesh or frame should therefore be treated as a warning that the retained fraction may contain more than genuinely oversized particles. This is especially relevant for fine polymer powders, pharmaceutical materials, chemical powders, and other materials prone to electrostatic charging. Why Wet Sieving Can Produce a Different Result Wet sieving can reduce problems associated with agglomeration, static electricity, or persistent mesh blockage. But wet sieving is not simply dry sieving with liquid added. The liquid becomes part of the test method. A suitable medium may improve dispersion, reduce static effects, and help fine particles pass through the sieve. At the same time, it may also alter the sample. Depending on the material and liquid, particles may dissolve, swell, soften, react chemically, or experience changes in surface behavior. A controlled wet-sieving method should therefore define the liquid medium, sample preparation, dispersing agents, rinsing procedure, drainage conditions, test duration, and endpoint criteria. The objective is not simply to make more material pass through the sieve. The laboratory should first determine whether high residue in dry sieving represents genuinely oversized particles or poor particle dispersion. For applications affected by static electricity, agglomeration, or wet-sieving conditions, our laboratory sieve shaker selection guide explains how these factors should be considered during equipment selection. Why Sieving Time and Endpoint Criteria Matter Sieving time can also change the reported result. Consider two laboratories testing the same powder with the same nominal sieve aperture. One runs the sieve shaker for five minutes. The other runs it for fifteen minutes. If material continues to pass through the sieve after the first five minutes, the two laboratories are not performing equivalent tests. Longer sieving may give particles more opportunities to reach an opening, change orientation, or separate from weak agglomerates. For this reason, instructions such as: “Sieve until it looks finished.” are unsuitable for comparative QC. When sieve analysis is used for batch release, supplier acceptance, or interlaboratory comparison, test duration or endpoint criteria should be defined in the SOP. The objective is reproducibility, not simply reducing the amount of material left above the sieve. Why Different Particle Size Methods Do Not Always Agree If two particle size reports disagree, one of the first questions should be whether the laboratories used the same measurement principle. A result expressed in micrometers does not necessarily represent the same physical quantity across different methods. Mechanical sieving determines whether a particle can pass through an opening of defined geometry under specified mechanical conditions. Laser diffraction evaluates light-scattering behavior and calculates an equivalent particle size distribution using an optical model. Dynamic image analysis evaluates projected particle images and can provide information related to both size and shape. These differences become especially important for irregular particles. An elongated particle may remain above a sieve when lying flat but pass through the same opening when it approaches at a different angle. Laser diffraction may report an equivalent diameter, while image analysis may describe length and width separately. The key point is: The same unit, μm, does not mean that different methods are measuring exactly the same physical quantity. This is why results generated by different techniques should not be compared without considering the measurement principle. Before Comparing Two Particle Size Reports, Check These 9 Conditions Before recalibrating an instrument, rejecting a batch, or questioning a supplier’s data, first determine whether the laboratories performed comparable tests. 1. Sample SourceWere the samples taken from the same batch using comparable sampling procedures? 2. Sample ConditionWere moisture level, storage conditions, and handling history comparable? 3. Sample PreparationWere drying, mixing, dividing, or other preparation procedures controlled? 4. Agglomeration and DispersionWas the material tested in a comparable and controlled physical state? 5. Measurement MethodDid both laboratories use the same analytical principle? 6. Wet or Dry ConditionsWas the powder tested under comparable environmental and dispersion conditions? 7. Sample QuantityWas a comparable amount of material introduced into each test? 8. Test DurationWere the same sieving or dispersion times used? 9. Endpoint CriteriaDid both laboratories use the same rule to determine when the test was complete? If these conditions differ, the reported particle size values may not be directly comparable even when both laboratories are operating their equipment correctly. How to Select Equipment Without Changing the Test Method The same logic should guide laboratory equipment procurement. A laboratory sieve shaker should not be selected first and then used to define the test method afterward. A more defensible sequence is: Understand powder behavior → Define the QC objective → Select the test method → Establish test conditions → Select equipment capable of repeating that method For free-flowing materials, conventional dry sieving may be appropriate. For powders affected by static electricity or agglomeration, sample preparation may need to be reconsidered, or wet sieving may need to be evaluated. For irregular particles, the mechanical motion of the sieve shaker can become part of the method. For very fine powders or applications requiring detailed particle size distributions, another analytical technique may be more suitable than mechanical sieving alone. Particle size data become useful when the conditions behind the numbers are understood. For procurement, R&D, and QC teams, reliable comparison requires more than matching the unit “μm” on two reports. It requires comparing the sample condition, test method, and operating procedure behind those numbers. When these conditions are controlled, particle size data become far more useful for batch comparison, supplier qualification, incoming quality control, process development, and material acceptance decisions.
    LEER MÁS
  • How to Choose an Ultrasonic Sieve Deblinding System: Specifications, Sizing & Testing Guide
    How to Choose an Ultrasonic Sieve Deblinding System: Specifications, Sizing & Testing Guide
    Oct 23, 2026
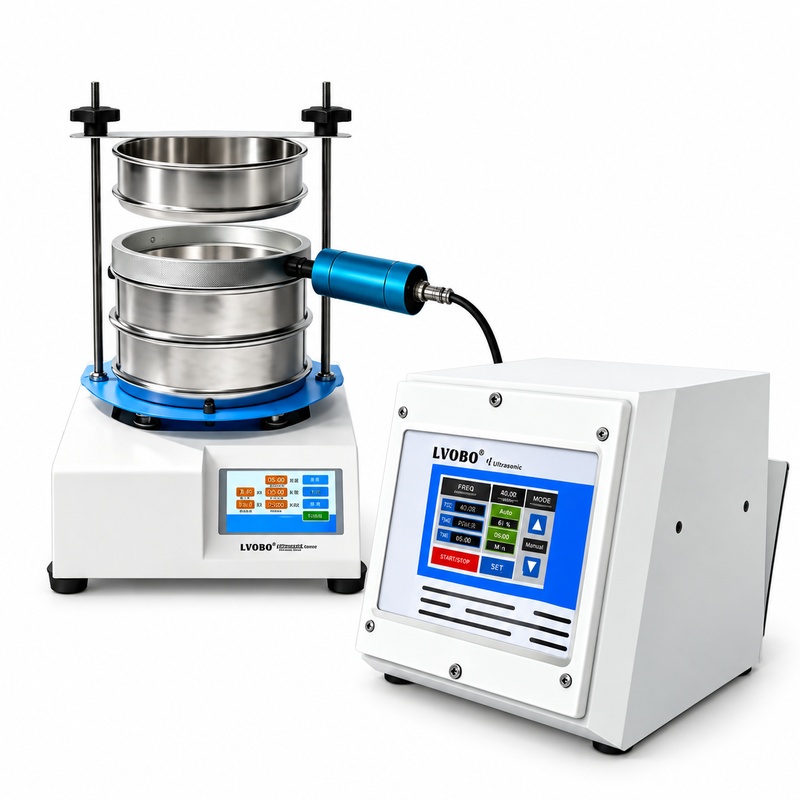
    Fine powder screening can become difficult when particles accumulate on sieve openings, restrict material flow, or form agglomerates during separation. These problems may increase screening time, require frequent mesh cleaning, and affect the consistency of particle classification. An ultrasonic sieve deblinding system can help address these challenges by introducing high-frequency vibration to the screening mesh. However, selecting the right system involves more than comparing frequency and power ratings. Sieve diameter, component matching, mesh specifications, equipment compatibility, and operating conditions all influence screening performance. This practical guide explains how ultrasonic deblinding works, how to choose between 200mm and 300mm sieve configurations, which technical specifications matter, and how to evaluate performance before purchasing. 1. What Is an Ultrasonic Sieve Deblinding System? An ultrasonic sieve deblinding system is designed to reduce mesh blockage during fine powder screening. It introduces high-frequency vibration to the screening mesh, helping prevent particles from accumulating in sieve openings and maintaining more effective screening conditions. A typical ultrasonic system consists of three main components: Ultrasonic Generator Produces the high-frequency electrical signal required to operate the ultrasonic screening system. Ultrasonic Transducer Converts the electrical signal into high-frequency mechanical vibration. Ultrasonic Sieve Frame Transfers ultrasonic vibration to the screening mesh and provides a suitable mounting structure. These components function together as a matched system. Importantly, ultrasonic deblinding is generally used alongside a compatible mechanical sieve shaker. The mechanical equipment provides the primary screening movement, while ultrasonic vibration assists in keeping the mesh openings clear. The two functions complement each other rather than replace one another. 2. Why Component Matching Matters More Than Power Alone A common mistake when selecting ultrasonic screening equipment is focusing primarily on the generator's power rating. In practice, a higher power specification does not automatically translate into better screening performance. Several factors affect how ultrasonic energy reaches the sieve mesh: Generator and transducer matching: The electrical characteristics of the generator must be compatible with the transducer. Operating frequency: The system must operate under suitable resonance conditions. Sieve frame design: The frame influences how vibration is transmitted to the screening mesh. Mesh installation: Mesh tension, construction, and aperture size can affect screening behavior. Mechanical integration: The ultrasonic assembly must fit and operate with the existing screening machine. Powder characteristics: Particle size, moisture, electrostatic behavior, and agglomeration can influence results. An improperly matched ultrasonic assembly may produce inconsistent screening performance even when the generator has a relatively high power rating. For this reason, buyers should evaluate the complete generator, transducer, and sieve frame arrangement rather than purchasing components solely according to power specifications. 3. Choosing Between 200mm and 300mm Ultrasonic Sieve Systems The appropriate sieve diameter depends on the existing screening equipment, sample quantity, available screening area, and installation requirements. The LVOBO BO-CSZ series is available in two configurations: BO-CSZ200: 200mm ultrasonic sieve frame. BO-CSZ300: 300mm ultrasonic sieve frame. Both configurations share the same ultrasonic generator specifications. 200mm vs. 300mm Selection Guide Selection Factor BO-CSZ200 BO-CSZ300 Sieve Diameter 200mm 300mm Sample Quantity Suitable to evaluate for smaller laboratory batches Worth considering for larger sample quantities Existing Sieve Shaker Requires compatible 200mm mounting arrangement Requires compatible 300mm mounting arrangement Screening Area Smaller nominal screening area Larger nominal screening area Installation Interface Verify mounting and clamping dimensions Verify mounting and clamping dimensions Continuous Operation Confirm operating limits Confirm operating limits Budget & Lead Time Request model-specific quotation Request model-specific quotation A 300mm sieve provides a larger nominal screening area than a 200mm sieve, but this does not automatically guarantee higher throughput. Actual screening performance depends on the mesh aperture, effective open area, powder behavior, sample loading, and mechanical screening conditions. Selection Tip: Start with the sieve diameter supported by your existing equipment. Then evaluate whether the available screening area meets your sample quantity and process requirements. 4. Key Technical Specifications to Review Technical specifications should be considered as part of the complete screening arrangement rather than as isolated values. The following table summarizes the LVOBO BO-CSZ ultrasonic sieve deblinding system. Technical Specifications Parameter Specification Models BO-CSZ200 / BO-CSZ300 System Type Ultrasonic Sieve Deblinding System Ultrasonic Frequency 28kHz Input Voltage AC100–220V Input Power 350W Power Adjustment Touchscreen percentage-based control Amplitude Independent Amplitude control Duty Cycle Setting 80%–100% Total Operating Time 0.1–999 min Ultrasonic ON Time 0.1–999 min Ultrasonic OFF Interval 0.1–999 min Temperature Alarm Setting 0–99°C Temperature Monitoring Real-time temperature display Temperature Protection Alarm notification Memory Presets 21 groups Cooling Design Transducer heat-dissipation design Sieve Configuration Single-Layer Sieve Screen Available Sieve Diameters Φ200mm / Φ300mm Electrical Connection Matched generator-to-transducer connection Generator Dimensions (D × W × H) 176 × 176 × 220mm Included Components Generator, matched transducer, and corresponding ultrasonic sieve frame Mechanical Sieve Shaker Not included Note: The generator dimensions refer to the control unit only, not the complete installed screening equipment. Sieve mesh specifications and additional accessories should be confirmed when ordering. Understanding the Control Functions Power and Amplitude The touchscreen provides percentage-based power adjustment. Amplitude is presented as a separate control function. The power percentage should not be interpreted as a calibrated amplitude measurement. Programmable Timing Operators can configure total operating time, ultrasonic ON time, and ultrasonic OFF interval independently. Each timing function supports settings from 0.1 to 999 minutes, providing flexibility for different screening procedures. 21 Memory Presets The system supports storage of up to 21 groups of operating settings. This allows operators to save and recall previously used configurations, reducing repetitive parameter setup during laboratory screening. Temperature Monitoring and Alarm The touchscreen displays the monitored temperature in real time. The alarm temperature can be configured from 0 to 99°C. When the set threshold is reached, the system provides an alarm notification to alert the operator. The alarm function should not be interpreted as automatic shutdown or automatic interruption of ultrasonic output. Duty Cycle The system provides a duty cycle setting range of 80%–100%. This setting describes an ultrasonic operating parameter and does not, by itself, establish that the equipment can operate continuously without interruption. For extended screening cycles, the permissible operating duration and thermal conditions should be checked. 5. Practical Features That Influence Daily Operation Technical performance is important, but day-to-day usability can also influence the suitability of a screening system. Press-Down Frame Access Some compatible screening arrangements use a press-down fixing structure to hold the sieve frame in position. When the fixing points are released, the sieve frame can be accessed for cleaning, inspection, or replacement. This can be particularly useful in laboratories where operators frequently change materials or sieve configurations. Before purchasing, confirm that the ultrasonic sieve frame and fixing arrangement are compatible with the existing mechanical sieve shaker. Matched Transducer and Heat Dissipation Ultrasonic transducers convert electrical energy into high-frequency mechanical vibration. Temperature rise during operation depends on the transducer design, operating settings, installation, and working conditions. The LVOBO BO-CSZ system uses a matched transducer with a heat-dissipation design intended to help manage heat buildup during screening. For applications involving extended operating cycles, actual operating temperature and permissible working duration should be evaluated under representative conditions. Touchscreen Operation and Saved Settings The touchscreen interface provides access to power, amplitude, timing, temperature monitoring, and memory functions. For laboratories working with multiple powder samples, saved parameter groups can help operators return to previously used screening settings. The ability to configure ultrasonic ON/OFF intervals also provides flexibility when developing different screening procedures. These functions are especially relevant when repeatability and clear operating procedures are important. 6. Essential Pre-Purchase Checklist Before purchasing an ultrasonic sieve deblinding system, buyers should prepare detailed information about their existing equipment and intended application. The following checklist can help reduce compatibility problems and unexpected installation requirements. A. Existing Screening Equipment 1. Sieve Shaker Manufacturer and Model Provide the manufacturer name, model number, and nominal sieve diameter. 2. Mounting Interface Supply photographs or technical drawings showing the sieve mounting area, fixing structure, and relevant dimensions. 3. Required Sieve Diameter Specify whether the application requires a 200mm or 300mm ultrasonic sieve frame. 4. Installation Clearance Check available space, frame height, clamping arrangement, and possible interference with other machine components. B. Electrical Requirements 5. Power Supply Confirm the available supply voltage, mains frequency, and destination-country requirements. 6. Plug Configuration Identify the required electrical plug type before shipment. 7. Protective Grounding Verify that the installation provides suitable protective earthing and follows the manufacturer's electrical instructions. 8. Cable Length and Connectors Confirm the transducer connection type, cable length, available routing space, and any required extension. C. Sieve Mesh and Powder Characteristics 9. Powder Type Record the material being screened and its relevant handling characteristics. 10. Particle Size Distribution Provide the approximate particle size range and target separation requirements. 11. Mesh Aperture Specify the required mesh number or opening size. 12. Wire Diameter and Open Area Where available, provide the mesh wire diameter and open-area percentage, especially for fine screening applications. 13. Mesh Tensioning Method Confirm how the mesh is installed, tensioned, and replaced. 14. Sample Quantity Record the expected sample mass per test and the frequency of screening operations. D. Operating Environment and Safety 15. Environmental Conditions Specify ambient temperature, humidity, ventilation, and dust exposure. 16. Screening Duration Provide the expected screening time per batch and the number of operating cycles per day. 17. Combustible Dust Hazards Identify whether the powder presents combustible dust or explosive-atmosphere risks. Never assume standard ultrasonic screening equipment is suitable for hazardous areas without an appropriate safety assessment. 18. Noise Requirements Confirm whether the installation has specific noise limitations or monitoring requirements. 19. Electromagnetic Compatibility For installations with sensitive instruments or special electrical requirements, review the relevant EMC considerations. E. Procurement and Delivery 20. Supply Scope Confirm the exact components included in the quotation, particularly the sieve mesh, electrical accessories, and mounting hardware. 21. Delivery and Packaging Request model-specific packaging dimensions, shipment weights, and estimated delivery schedules. 22. Technical Support Confirm the availability of operating instructions, installation guidance, maintenance information, and troubleshooting assistance. Preparing this information before ordering helps suppliers review the application more accurately and recommend a suitable equipment configuration. 7. LVOBO BO-CSZ200 and BO-CSZ300 Configurations The LVOBO BO-CSZ series combines an ultrasonic generator, matched transducer, and dedicated sieve frame into a coordinated screening system. Configuration BO-CSZ200 BO-CSZ300 Ultrasonic Generator Included Included Matched Transducer Included Included Ultrasonic Sieve Frame Φ200mm Φ300mm Operating Frequency 28kHz 28kHz Duty Cycle Setting 80%–100% 80%–100% Memory Presets 21 groups 21 groups Temperature Alarm Included Included Generator Dimensions 176 × 176 × 220mm 176 × 176 × 220mm Mechanical Sieve Shaker Not included Not included Sieve mesh specifications, mounting compatibility, and additional accessories should be confirmed when requesting a quotation. 8. How to Validate Ultrasonic Screening Performance The most reliable way to evaluate ultrasonic assistance is to test representative material under controlled conditions. Whenever practical, compare conventional mechanical sieving with ultrasonic-assisted sieving while keeping other screening variables consistent. Step 1 — Prepare Representative Powder Samples Use material that reflects the intended application. Record: Powder type Initial sample mass Particle size characteristics Moisture condition Required sieve aperture Ambient testing conditions Avoid comparing samples with significantly different properties. Step 2 — Establish a Baseline Perform a screening test using the mechanical sieve shaker without ultrasonic assistance. Record the operating settings, screening time, and material behavior. Pay attention to particle buildup, blocked mesh openings, and material remaining on the sieve. Step 3 — Repeat with Ultrasonic Assistance Repeat the test with the ultrasonic system enabled. Keep the same sample loading, mesh aperture, mechanical screening settings, and defined screening endpoint wherever possible. For reliable comparisons, repeat each test condition several times. Step 4 — Record Key Performance Indicators Indicator Measurement Evaluation Purpose Screening Time Time to reach the same defined screening endpoint Evaluates process duration Material Recovery Recovered material mass relative to initial mass Identifies material loss or retention Mesh Blockage Percentage or estimated proportion of blocked apertures Evaluates deblinding effectiveness Cleaning Time Time needed to restore the sieve to a defined clean condition Evaluates cleaning effort Temperature Rise Temperature change at a consistent measurement point Evaluates thermal behavior Repeatability Variation between repeated tests Evaluates screening consistency Step 5 — Compare the Results Evaluate the measurements together rather than relying on a single performance indicator. For example, a shorter screening time is not necessarily beneficial if material recovery decreases or the required particle separation is affected. Similarly, reduced mesh blockage should be considered alongside equipment temperature, cleaning requirements, and repeatability. Practical Recommendation: Use a consistent test method and record the ultrasonic operating settings so results can be compared and repeated. Saved parameter groups can help operators return to previously used settings during laboratory trials. 9. Applications That Require Additional Caution Ultrasonic deblinding can be useful in many fine powder screening applications, but not every material or operating environment is suitable. High-Moisture Powders High moisture levels can increase particle adhesion and create strong agglomerates. Ultrasonic vibration alone may not resolve moisture-related blockage. Material conditioning or another processing method may be necessary. Strongly Electrostatic Powders Electrostatic attraction can cause powder particles to adhere to the mesh and surrounding surfaces. Additional static-control and handling measures may be required. Highly Agglomerated Materials Strongly bonded agglomerates may require preconditioning before effective sieving. Ultrasonic assistance should not be assumed to break down every type of agglomerate. Combustible Metal Powders Fine combustible metal powders can present serious fire and explosion hazards. Equipment suitability, installation conditions, and appropriate dust-safety measures must be evaluated before use. Corrosive Chemical Powders Corrosive powders require careful review of their suitability for the equipment and intended operating conditions. Continuous Production A system suitable for laboratory screening is not automatically suitable for uninterrupted industrial production. Continuous-duty applications require separate evaluation of thermal behavior, operating limits, maintenance requirements, and installation conditions. The 80%–100% duty cycle setting should not be interpreted as proof of continuous-duty capability. Frequently Asked Questions Can a larger sieve diameter improve screening throughput? A larger sieve can provide more nominal screening area, but actual throughput depends on mesh aperture, sample loading, powder properties, and operating conditions. Representative testing is recommended. Can I reuse my existing sieve mesh? This depends on the mesh dimensions, construction, tensioning method, and the ultrasonic frame design. Compatibility should be confirmed before attempting installation. Can saved operating settings be used for repeated laboratory screening? Yes. The system supports 21 groups of memory presets, allowing previously saved operating settings to be recalled. Does ultrasonic deblinding eliminate all mesh blockage? No. Ultrasonic assistance helps reduce mesh blinding, but performance depends on the powder characteristics, sieve specifications, and operating conditions. What should I do if screening results are inconsistent? Check sample preparation, mesh condition, material loading, transducer installation, operating settings, and mechanical sieve shaker performance. Repeat testing under consistent conditions to identify possible causes. Conclusion Selecting an ultrasonic sieve deblinding system should begin with three questions: Is the ultrasonic frame compatible with the existing sieve shaker? Is the selected diameter appropriate for the powder sample and required screening area? Can representative testing demonstrate a meaningful improvement in screening performance? Answering these questions helps buyers evaluate a complete screening solution rather than relying on individual specifications. Need Help Choosing Between BO-CSZ200 and BO-CSZ300? Share your powder type, required sieve diameter, mesh size, existing sieve shaker model, and intended application. LVOBO can help review the configuration requirements for your screening equipment. Email: lvobo2026@gmail.com WhatsApp: +86 13235024070Prepared by the LVOBO Application Engineering Team — specialists in ultrasonic screening system configuration and fine powder processing support.
    LEER MÁS
  • What Is a Laboratory Sieve Shaker? Working Principle, Applications, and Selection Guide
    Oct 05, 2026
    In research, quality control, and production testing involving powders, granules, and raw materials, particle size distribution can directly affect flowability, dissolution rate, mixing uniformity, reaction efficiency, and final product quality. For laboratories in industries such as chemicals, pharmaceuticals, food, advanced materials, and scientific research, achieving fast, stable, and repeatable particle separation is a fundamental but important task. A laboratory sieve shaker is designed for exactly this purpose. By using mechanical vibration, electromagnetic vibration, or multidirectional motion, a sieve shaker moves a sample through a stack of test sieves with different mesh sizes. This allows particles to be classified according to size and helps laboratories determine the percentage of material within different particle-size ranges. What Is a Laboratory Sieve Shaker? A laboratory sieve shaker is an instrument used for particle size analysis, grading, and sieve residue testing of powders and granular materials. In a typical test, several standard test sieves with different aperture sizes are stacked from coarse to fine. The sample is placed on the top sieve. Once the machine starts, continuous vibration causes the material to move, spread, and pass through the sieve openings. Larger particles remain on the upper sieves, while smaller particles gradually pass through to the lower layers. After the sieving process is completed, the material retained on each sieve can be weighed to calculate the percentage of particles within each size range. Laboratory sieve shakers are commonly used for: Particle size distribution analysis Raw material particle size testing Product quality control Sieve residue analysis Impurity ratio testing New material development Formulation and process optimization Compared with manual sieving, a laboratory sieve shaker can improve testing efficiency while reducing operator-dependent variation. How Does a Laboratory Sieve Shaker Work? The purpose of a sieve shaker is not simply to make the sieve vibrate. Its main function is to create an effective particle movement pattern on the sieve surface so that particles can separate efficiently according to size. During the sieving process, the material usually goes through three basic stages. 1. Sample Dispersion Vibration helps break up the material bed and spread particles across the sieve surface. This allows more particles to come into contact with the sieve openings. 2. Passage Through the Sieve Openings When a particle is smaller than the sieve aperture and approaches the opening at a suitable orientation, it can pass through to the next sieve. 3. Particle Size Classification As the process continues, particles of different sizes are gradually retained on different sieve levels, producing a classified particle-size distribution. Different laboratory sieve shakers use different vibration mechanisms. Some machines use vibration motors to generate mechanical motion, while electromagnetic sieve shakers use an electromagnetic excitation system to create high-frequency reciprocating vibration. Vibration intensity, sieving time, and particle movement pattern can all influence sieving efficiency and test repeatability. Why Is Repeatability Important in Laboratory Sieving? For laboratory testing, simply separating the material is usually not enough. A more important question is: Can the same sample produce similar results when tested under the same conditions? If vibration intensity, sieving time, or operating procedures vary from test to test, the results may also vary significantly. This is why modern laboratory sieve shakers increasingly use programmable and adjustable operating parameters. For example, LVOBO laboratory sieving equipment allows users to adjust operating parameters for different materials and store commonly used sieving programs. When the same material needs to be tested again, operators can quickly recall previously established settings. This reduces repeated parameter adjustment and helps laboratories create more standardized testing procedures. Such functionality is particularly useful for R&D laboratories, quality-control laboratories, and companies that perform regular batch testing. What Materials Can Be Tested with a Laboratory Sieve Shaker? Laboratory sieving equipment can be used for a wide range of powders and granular materials. Chemical Materials Examples include resin powders, pigments, coating powders, chemical raw materials, and functional powders. Particle size can affect dispersion, reaction performance, processing behavior, and product consistency. Pharmaceutical and Biopharmaceutical Materials Drug powders, excipients, and certain granular formulations often require particle size control during development and production. A controlled particle size distribution can contribute to more consistent product performance. Food Materials Flour, starch, seasonings, food additives, sugar powder, and other food powders can be tested for particle size or impurities using laboratory sieving equipment. Advanced Materials Applications include metal powders, ceramic powders, battery materials, 3D-printing powders, and other functional materials. For many of these materials, particle size distribution is closely related to downstream processing performance. Universities and Research Laboratories Research institutes and universities can use laboratory sieve shakers for material development, particle analysis, formulation studies, and process validation. Minerals, grains, plastic granules, and many other particulate materials can also be tested depending on the specific application. How to Choose the Right Laboratory Sieve Shaker When selecting a laboratory sieve shaker, it is not enough to compare only machine power or price. The selection should be based on the sample characteristics and testing requirements. 1. Particle Size Range First, determine the particle size range that needs to be analyzed. Different test sieves have different aperture sizes, so the sieve specifications should match the target particle-size range. For a wide distribution, multiple sieves with different mesh sizes can be stacked together. 2. Sieve Diameter Standard laboratory test sieves are available in different diameters. Before selecting a machine, confirm that it is compatible with the test sieve sizes already used in your laboratory or planned for future use. 3. Sample Quantity The amount of material used in one test may range from only a few grams to several hundred grams or more. Excessive loading can reduce sieving efficiency, so the machine and sieve diameter should be selected according to the typical sample quantity. 4. Vibration Method Different vibration systems provide different operating characteristics. Traditional vibration-motor systems are widely used and suitable for many routine laboratory sieving applications. Electromagnetic sieve shakers use high-frequency electromagnetic excitation and can be suitable for applications requiring precise vibration control and good repeatability. 5. Adjustable Parameters Different powders may require different sieving conditions. A machine that allows users to adjust vibration intensity, operating time, and vibration mode provides greater flexibility for optimizing the process for different materials. 6. Program Storage If a laboratory regularly tests several standard materials, program memory can significantly improve efficiency. Operators can save different sieving parameters for different materials and recall them during future tests. This can also support the development of standardized operating procedures, or SOPs. Why Are Multiple Test Sieves Important? Laboratory particle size analysis is usually not just about determining whether particles are “large” or “small.” The goal is often to understand the full particle size distribution. For example, a sieve stack may be arranged as follows: 500 μm↓250 μm↓125 μm↓63 μm↓Receiving Pan After sieving, particles within different size ranges remain on different sieves. By weighing the material retained on each sieve, the percentage of each fraction can be calculated. A common calculation is: Sieve Retention (%) = Weight Retained on the Sieve ÷ Total Sample Weight × 100% This provides a clearer picture of the particle-size composition of the sample. For product development and quality control, such data are generally more useful than evaluating powder appearance alone. How Can You Improve the Reliability of Laboratory Sieving Results? To obtain more consistent results, important testing conditions should remain as stable as possible. Recommended practices include: Use test sieves of the same specification and condition Maintain a consistent sample weight Use a fixed sieving time Keep vibration settings consistent Prevent excessive sieve blockage Clean sieves regularly Establish standard testing programs for recurring materials Some powders may also be prone to agglomeration, static electricity, or irregular particle behavior. For these materials, additional optimization of the sieving parameters may be required. There is no single vibration setting that works perfectly for every powder. For this reason, establishing a dedicated sieving program for each material through repeated testing can help improve data consistency. LVOBO Laboratory Sieving Solutions LVOBO focuses on the development and manufacture of laboratory sieving equipment and related laboratory instruments. To meet different particle-testing requirements, we provide multiple laboratory sieving solutions, including vibratory sieve shakers and electromagnetic sieve shakers. LVOBO's latest laboratory vibratory sieve shakers feature touchscreen control and adjustable operating parameters. Depending on the material, users can adjust forward motion, reverse motion, vertical vibration, operating time, and cycle settings. The system also supports storing multiple commonly used sieving programs. When the same or similar material is tested again, operators can quickly recall previous settings, reducing repetitive setup work. For applications requiring high-frequency vibration, the LVOBO BO-300ESS Electromagnetic Sieve Shaker uses an electromagnetic excitation system to generate high-frequency reciprocating motion. Its vibration amplitude, vibration interval, and sieving time can be adjusted according to different testing requirements. Different sieving technologies are suitable for different laboratory conditions. For this reason, we recommend selecting a sieve shaker based on the sample type, target particle size, sieve specifications, sample quantity, and testing workflow rather than evaluating the machine only by power or vibration amplitude. Conclusion Particle size is one of the most important basic parameters for powders and granular materials. A suitable laboratory sieve shaker does more than simply separate particles. More importantly, it helps laboratories establish a stable and repeatable particle-size testing process. Before choosing a sieve shaker, consider the following questions: What material do you need to sieve? What particle-size range do you need to analyze? What diameter of standard test sieve will you use? How much material will you test each time? Do you need to save and recall sieving programs? Selecting equipment based on these factors is usually more effective than comparing only power, amplitude, or price. If you are looking for laboratory sieving equipment for powders, granules, or particle size analysis, contact LVOBO. Our team can help you select a suitable laboratory sieving solution based on your sample type, sieve specifications, and testing requirements.
    LEER MÁS
  • Why Fine Powders Blind Test Sieves—and How an Ultrasonic Test Sieve Shaker Helps
    Why Fine Powders Blind Test Sieves—and How an Ultrasonic Test Sieve Shaker Helps
    Jul 14, 2026
      Fine Powder Screening Guide Why Fine Powders Blind Test Sieves—and How an Ultrasonic Test Sieve Shaker Helps Sieve analysis looks straightforward when a material is dry, free-flowing and substantially smaller than the selected openings. The procedure becomes much less predictable when the sample contains fine, cohesive or electrostatic particles. Instead of presenting themselves individually to the mesh, particles form agglomerates, adhere to the wires and progressively cover usable openings. The operator may extend the test, increase mechanical vibration or stop repeatedly to brush the mesh, yet the result can remain slow and difficult to reproduce. An ultrasonic test sieve shaker addresses this specific limitation by combining conventional laboratory sieve motion with high-frequency energy applied to one dedicated sieve frame. The mechanical shaker continues to move the full sieve stack, while the ultrasonic generator, matched transducer and connected frame target the layer where mesh blinding is most likely to occur. The goal is not to replace a sound test method or guarantee a clog-free result. It is to keep more of the critical mesh area active and make difficult fine-powder screening easier to control. In This Guide Why fine powders blind sieve mesh Where mechanical screening reaches its limit How ultrasonic-assisted sieving works What changes in the screening process Applications in research and advanced materials How to select a suitable system Method-development recommendations Test-sieve standards and result comparability Frequently asked questions Key Takeaways Fine powders can blind mesh because cohesion, electrostatic behavior, particle shape and loading can prevent individual particles from reaching open apertures. Mechanical horizontal and vertical motion remains responsible for moving the complete sieve stack and separating ordinary powders and granules. Ultrasonic assistance introduces high-frequency vibration directly into one dedicated sieve frame at the most difficult separation point. The most defensible benefits are reduced blinding, improved dispersion and more consistent screening—not “zero clogging” or guaranteed analytical accuracy. Method repeatability still depends on representative sampling, verified test sieves, controlled sample mass, documented settings and consistent cleaning. Why Do Fine Powders Blind Test-Sieve Mesh? Coarse, free-flowing particles are dominated largely by gravity and collision. Fine powders behave differently because their mass decreases faster than the relative influence of surface forces. Cohesion between particles, electrostatic charging, moisture, irregular morphology and soft agglomeration can therefore become more important than gravity. A nominally fine sample may reach the sieve as clusters rather than as discrete particles. Mesh blinding occurs when particles lodge in apertures, bridge across openings or build a persistent layer on the wire cloth. Once part of the mesh is covered, the effective screening area shrinks. Material then concentrates on the remaining open area, increasing local loading and making further blockage more likely. This feedback loop explains why a test may start normally and then slow dramatically. Aperture size alone does not predict the difficulty. Two powders with similar nominal particle-size distributions can behave very differently because of particle shape, surface texture, density, oxidation, humidity or formulation additives. Gas-atomized metal powder may flow differently from water-atomized powder. A dry ceramic powder may behave differently after storage. A pharmaceutical blend may contain a small cohesive fraction that controls the behavior of the whole sample. Experimental work on vibrated fine-powder beds illustrates this broader point. Studies by Sonar and Katsuragi observed consolidation, fracture and decompaction behavior in cohesive micron-scale powder under different vibration conditions. Their work concerns powder-bed vibration rather than ultrasonic sieving, but it reinforces an important practical lesson: cohesive fine powders do not respond like free-flowing grains, and simply applying “more shaking” does not create one universal outcome. See the authors’ original studies on decompaction-wave propagation and vibration-induced fluidization of fine powder. Where a Conventional Laboratory Test Sieve Shaker Reaches Its Limit A well-designed laboratory test sieve shaker is still the foundation of the process. Horizontal forward/reverse rotation distributes material across the sieve surface, while vertical vibration lifts and reorients particles so that they can approach apertures in different orientations. With suitable test time, sample mass and sieve selection, this combined motion is effective for many powders and granules. The limitation appears when mechanical motion moves the stack but cannot keep the critical fine mesh clear. Increasing time may only circulate an agglomerated layer. Increasing intensity can sometimes compact material against the mesh, accelerate sieve wear or change the balance between passage and retention. Manual brushing interrupts the method and introduces another operator-dependent variable. Adding dispersing aids can alter the sample and may be unacceptable for research, pharmaceutical or high-purity material workflows. The useful question is therefore not “Is ultrasonic always better?” It is “At which sieve layer does adhesion or blinding prevent the mechanical method from completing its intended separation?” An ultrasonic system is most valuable when that critical layer can be identified and fitted with a dedicated ultrasonic frame. How Does an Ultrasonic Test Sieve Shaker Work? An ultrasonic-assisted laboratory system contains two coordinated but distinct sources of motion. Understanding their roles prevents unrealistic expectations and helps the laboratory design a repeatable procedure. 1. The Mechanical Shaker Moves the Entire Stack The shaker provides the conventional screening action for every installed sieve: horizontal forward/reverse movement plus vertical vibration. It carries the sample across successive apertures and collects size fractions in the appropriate pans. Touchscreen models can store operating programs so laboratories can document and recall speed, intensity, frequency, run count and motion timing for repeated procedures. 2. The Ultrasonic Generator Produces High-Frequency Output The separate generator produces a controlled high-frequency electrical signal. In the LVBO configuration discussed here, the nominal output frequency is 28 kHz, with adjustable amplitude and a touchscreen display for time, temperature and power information. Frequency is a system specification; it should not be interpreted as a test-sieve standard or a guarantee that every material will respond identically. 3. A Matched Transducer Transfers Energy The transducer converts the generator’s electrical output into mechanical ultrasonic vibration and transfers that energy through its connection to the dedicated sieve frame. Matching the generator, transducer, connection and frame matters because losses or unstable coupling can reduce the energy that reaches the mesh. 4. One Dedicated Frame Targets the Critical Layer In this product configuration, ultrasonic energy is applied to one dedicated ultrasonic sieve frame per system. The other sieves still receive the shaker’s mechanical motion. This focused architecture lets the laboratory position ultrasonic assistance at the layer most vulnerable to blinding rather than implying that every sieve in a tall stack is ultrasonically energized. What Changes When Ultrasonic Assistance Is Added? More Active Screening Area High-frequency vibration at the mesh can make it harder for fine particles to remain lodged in openings or attached as a persistent layer. Keeping more apertures active supports continued passage at the critical separation point. The appropriate claim is “reduced mesh blinding,” not “zero clogging,” because performance remains material- and method-dependent. Improved Dispersion of Soft Agglomerates Ultrasonic energy can help disturb weakly bound clusters and reduce the residence time of powder on the mesh. That can be useful for electrostatic, low-density or cohesive powders that otherwise travel as lumps. It should not be assumed to deagglomerate every strongly bonded particle or to replace a separate sample-dispersion step when the method requires one. More Consistent Test Completion If blinding is the main cause of an incomplete or excessively long test, keeping the selected frame active can reduce operator intervention and make endpoint behavior more consistent. Repeatability still depends on the complete method: sample preparation, sieve condition, loading, operating parameters, duration, environmental control and cleaning. Better Control Than Simply Increasing Mechanical Intensity Ultrasonic assistance adds energy where the problem occurs—the selected mesh—without requiring the laboratory to drive the entire stack more aggressively. This can be a more targeted response than extending test time or increasing overall mechanical intensity. The optimum amplitude should be established experimentally for each material rather than automatically set to maximum. Where Is Ultrasonic-Assisted Sieving Most Useful? Metal Powders and Additive Manufacturing Metal powder particle size analysis supports incoming inspection, powder-lot comparison, reclaimed-powder monitoring and research into process consistency. Fine or irregular fractions can adhere to mesh, while high-density particles place significant load on the sieve. An ultrasonic frame can be positioned at the critical cut point to support metal-powder classification. Research on vibratory feeding of gas- and water-atomized metal powders also demonstrates that powder type and operating parameters materially affect flow behavior; see the original additive-manufacturing study by Sinclair and colleagues on vibratory powder feeding. Battery Materials and New-Material Research Cathode, anode, conductive and precursor powders may be fine, electrostatic or sensitive to contamination. Research teams often need controlled separation for material preparation, comparative studies or quality checks. Stainless-steel material-contact components and documented cleaning procedures should be evaluated against the chemistry and contamination limits of the specific sample. Pharmaceutical and Food Powders Fine excipients, active ingredients, nutraceutical powders and milled food ingredients may bridge or agglomerate. Ultrasonic sieving can support development and quality-control studies, but equipment suitability does not by itself establish GMP compliance, hygienic qualification or product-contact compatibility. Those requirements must be assessed within the buyer’s validated process. Chemical Materials, Pigments and Mineral Powders Pigments, catalysts, fillers, coatings, mineral powders and fine chemical intermediates frequently combine small particle size with irregular shape or electrostatic behavior. An ultrasonic screening machine can help laboratories complete difficult sieve cuts with less manual intervention, provided the material is compatible with the sieve, seals, transducer assembly and cleaning method. Electronic Ceramics and Laboratory Testing Alumina, zirconia and other electronic-ceramic powders require controlled handling because small fractions can affect forming and sintering behavior. Universities and materials laboratories can use sieve-based classification as one part of a broader characterization workflow, particularly when a physical retained fraction is needed for weighing, microscopy or subsequent testing. How to Select Fine Powder Sieving Equipment Selection should begin with the material and method, not with the largest available power value. Ask suppliers to evaluate the target cut size, particle morphology, density, sample mass, expected throughput, electrostatic tendency, moisture sensitivity and cleaning requirements. Identify the Critical Ultrasonic Layer Determine which aperture is actually blinding. Because this system uses one dedicated ultrasonic frame, it should be installed at the critical separation point. If several layers experience severe blinding, the method may require sequential tests, a different stack arrangement or a separate evaluation rather than an assumption that one transducer energizes every layer equally. Choose 200 mm or 300 mm A 200 mm configuration is compact and appropriate for many research-scale samples. A 300 mm configuration provides greater screen area and may suit larger samples or applications that benefit from lower areal loading. Diameter alone does not determine throughput; powder behavior, aperture, sample mass and acceptable endpoint remain important. Check Generator and Laboratory Compatibility Confirmed LVBO ultrasonic generator specifications Models BO-CSZ200 / BO-CSZ300 Input voltage AC100–220V Input power 350W Approximate output power 300W Output frequency 28kHz Generator dimensions 176 × 176 × 220 mm Dedicated ultrasonic frames 1 per system Frame options 200 mm / 300 mm Confirm local voltage, plug, grounding and laboratory electrical requirements before shipment. US, EU, UK and AU plug preparation may be available, but the laboratory remains responsible for confirming local installation and safety requirements. A Practical Method-Development Workflow Define the analytical objective. Specify the fractions or critical aperture, acceptable sample mass and how the retained material will be reported. Prepare a representative sample. Follow the laboratory’s sampling and conditioning procedure. Do not assume the shaker can correct sampling bias. Inspect and clean the sieves. Check wire cloth, frame, seals and ultrasonic connection. Damaged or contaminated sieves compromise results regardless of the drive system. Install the dedicated ultrasonic frame at the critical layer. Confirm that the transducer and cable are correctly secured before energizing the generator. Begin with conservative settings. Establish suitable mechanical motion, time and ultrasonic amplitude through controlled trials. Maximum intensity is not automatically the best setting. Document the complete recipe. Record sample mass, sieve stack, environmental conditions, mechanical parameters, ultrasonic amplitude, duration and endpoint criteria. Assess repeatability. Run replicate tests and compare retained masses, completion time and visible blinding. Optimize one variable at a time. Create cleaning and inspection intervals. Fine powder can accumulate at joints and mesh edges. Follow the manufacturer’s instructions and the laboratory’s contamination-control procedure. Safety note: Fine powders may present inhalation, reactivity, electrostatic or combustible-dust hazards. Review the material safety data, grounding, ventilation and dust-control requirements before testing. Do not process combustible or reactive powders unless the complete equipment and facility are approved for that hazard. Follow the operating manual and local laboratory rules. Test-Sieve Standards and Result Comparability Ultrasonic assistance cannot compensate for an unverified or damaged sieve. Test-sieve standards address the wire cloth, aperture tolerances, frame construction and inspection methods that underpin sieve-based particle classification. ASTM E11-24 covers woven-wire test-sieve cloth and test sieves used to classify materials by particle size. ASTM states that the specification includes requirements for sieve cloth, test-sieve construction and inspection procedures, with nominal apertures from 125 mm down to 20 µm. ISO 3310-1:2016 specifies technical requirements and test methods for test sieves of metal wire cloth over the same nominal aperture range and remains current after confirmation in 2022. These standards do not certify that an ultrasonic shaker will produce a particular result for every powder. They establish requirements for the sieve itself. Buyers should therefore phrase procurement requirements carefully: matching sieve pans can be configured to the requested ASTM E11 or ISO 3310-1 specification, while the screening method must still be developed and verified for the material. Is an Ultrasonic Sieve Shaker a Particle Size Analyzer? It is more accurate to describe the system as sieve-based particle size analysis equipment. The instrument separates material physically through specified apertures, allowing the laboratory to weigh retained fractions. A laser-diffraction or image-based particle size analyzer uses a different measurement principle and may report an equivalent diameter rather than a physical sieve fraction. The methods can be complementary. A particle size analyzer can provide rapid distribution data, while a laboratory vibratory sieve shaker can prepare fractions, remove oversize contamination or provide material retained at a defined aperture for further examination. Results from different principles should not be treated as interchangeable without a correlation study. LVBO’s Combined Mechanical and Ultrasonic Screening System LVBO combines BO-200SY or BO-300SY touchscreen laboratory shakers with BO-CSZ200 or BO-CSZ300 ultrasonic generators and one matching 200 mm or 300 mm dedicated frame. The shaker supplies programmable horizontal and vertical screening motion for the complete stack. The separate 28 kHz system adds adjustable ultrasonic assistance at the critical fine-powder layer. This architecture is intended for laboratories that need ordinary sieve separation and targeted anti-blinding assistance in one workflow. Before selection, share the material, target aperture, sample mass, current problem and destination voltage. A supplier evaluation or material trial is more useful than relying only on a generic mesh-number claim. Frequently Asked Questions What is an ultrasonic test sieve shaker? It is a laboratory sieve shaker combined with an ultrasonic generator, matched transducer and dedicated sieve frame. Mechanical motion moves the sieve stack, while high-frequency energy assists the selected mesh layer. Does ultrasonic screening completely eliminate mesh blinding? No universal system can guarantee zero blinding for every powder. Ultrasonic assistance is designed to reduce persistent adhesion and blockage. Performance depends on material behavior, aperture, loading, amplitude and test method. Can one ultrasonic generator energize every sieve in the stack? In the configuration described here, one dedicated ultrasonic frame is connected per system. The mechanical shaker moves the entire stack, but ultrasonic energy is focused on the selected frame. Why use 28 kHz? 28 kHz is the nominal output frequency of this matched LVBO generator and transducer system. It identifies the equipment configuration; it is not a test-sieve standard or a guarantee of identical performance for all materials. Should I choose a 200 mm or 300 mm sieve? Choose according to sample mass, available bench space, required screen area and existing laboratory method. A 300 mm frame offers more area, while a 200 mm system is more compact. Which powders are suitable? Typical candidates include cohesive or electrostatic metal, battery, ceramic, pharmaceutical, food, chemical, pigment and mineral powders. Compatibility and safety must be reviewed for the specific sample. Can ultrasonic sieving replace a laser particle size analyzer? Not directly. Sieve analysis produces physical mass fractions based on aperture passage. Laser diffraction uses an optical model. The methods can complement each other but measure particle size differently. What information should I send when requesting a recommendation? Provide the material name, target aperture or sieve standard, approximate particle-size range, sample mass, current blinding problem, desired frame diameter, destination voltage and any contamination or safety constraints. Need to Evaluate a Difficult Powder? Send LVBO your material, target sieve aperture, sample mass, existing test method and the type of blinding you observe. We can help you compare 200 mm and 300 mm configurations and identify the most appropriate layer for one dedicated ultrasonic frame. Request a material and configuration review before ordering. Technical References ASTM E11-24: Standard Specification for Woven Wire Test Sieve Cloth and Test Sieves. ISO 3310-1:2016: Test sieves—Technical requirements and testing—Part 1: Test sieves of metal wire cloth. Sonar, P. and Katsuragi, H. Decompaction-wave propagation in a vibrated fine powder bed. Sonar, P. and Katsuragi, H. Fracturing-induced fluidization of vibrated fine-powder column. Sinclair, C. W. et al. Vibratory Powder Feeding for Powder Bed Additive Manufacturing Using Water- and Gas-Atomized Metal Powders. { "@context": "https://schema.org", "@type": "FAQPage", "mainEntity": [ { "@type": "Question", "name": "What is an ultrasonic test sieve shaker?", "acceptedAnswer": {"@type": "Answer", "text": "It is a laboratory sieve shaker combined with an ultrasonic generator, matched transducer and dedicated sieve frame. Mechanical motion moves the sieve stack, while high-frequency energy assists the selected mesh layer."} }, { "@type": "Question", "name": "Does ultrasonic screening completely eliminate mesh blinding?", "acceptedAnswer": {"@type": "Answer", "text": "No universal system can guarantee zero blinding. Ultrasonic assistance is designed to reduce persistent adhesion and blockage, with performance depending on the material and method."} }, { "@type": "Question", "name": "Can one ultrasonic generator energize every sieve in the stack?", "acceptedAnswer": {"@type": "Answer", "text": "In this configuration, one dedicated ultrasonic frame is connected per system. Mechanical motion acts on the entire sieve stack."} }, { "@type": "Question", "name": "Why use 28 kHz?", "acceptedAnswer": {"@type": "Answer", "text": "28 kHz is the nominal output frequency of the matched LVBO generator and transducer configuration. It is not a test-sieve standard or a universal performance guarantee."} }, { "@type": "Question", "name": "Should I choose a 200 mm or 300 mm sieve?", "acceptedAnswer": {"@type": "Answer", "text": "Choose according to sample mass, bench space, required screen area and the established laboratory method."} }, { "@type": "Question", "name": "Which powders are suitable?", "acceptedAnswer": {"@type": "Answer", "text": "Typical candidates include cohesive or electrostatic metal, battery, ceramic, pharmaceutical, food, chemical, pigment and mineral powders, subject to compatibility and safety review."} }, { "@type": "Question", "name": "Can ultrasonic sieving replace a laser particle size analyzer?", "acceptedAnswer": {"@type": "Answer", "text": "Not directly. Sieve analysis produces physical mass fractions based on aperture passage, while laser diffraction uses an optical measurement model."} }, { "@type": "Question", "name": "What information should I send when requesting a recommendation?", "acceptedAnswer": {"@type": "Answer", "text": "Provide the material, target aperture, particle-size range, sample mass, current blinding problem, frame diameter, destination voltage and safety constraints."} } ] }
    LEER MÁS
  • Green Innovation of Powder Spraying Machine: Eco-friendly Development of Low-carbon Coating Era
    May 12, 2026
    Environmental protection and low-carbon have become the inevitable theme of global industrial manufacturing transformation, and powder spraying machines, as key equipment for surface coating, are leading the coating industry to bid farewell to high-pollution and high-energy consumption with continuous green technological innovation, opening a new chapter of sustainable production. Traditional liquid coating processes rely heavily on organic solvents, which will produce a large amount of volatile organic compounds (VOCs) during construction, causing air pollution and also bringing hidden dangers to the occupational health of operators. As a representative of green coating equipment, modern powder spraying machines completely abandon solvent-based raw materials and adopt solvent-free powder coatings, achieving near-zero VOC emissions fundamentally, which perfectly complies with increasingly stringent global environmental protection policies. The optimization of powder recovery system is the core highlight of green innovation of powder spraying machines. Traditional equipment has a low powder utilization rate, and a large amount of excess powder drifts away with the air flow, which not only causes serious material waste, but also pollutes the workshop environment. The new generation of powder spraying machines adopts closed-loop recycling design and high-efficiency dust purification structure, which can recover excess floating powder to the greatest extent, with the powder utilization rate exceeding 95%. The recycled powder can be reused after simple filtering, which greatly reduces production costs while cutting waste emissions. Energy-saving technological innovation runs through the whole operation link of the equipment. Modern powder spraying machines adopt low-power electrostatic control modules and optimized air duct design, effectively reducing electric energy loss during operation. Matching with low-temperature curing technology, it lowers the required curing temperature of powder coatings, shortens heating time, reduces the energy consumption of curing ovens by more than 25%, and realizes double energy saving in spraying and curing links. In addition, the structural design of the equipment also adheres to the green concept. The application of wear-resistant and corrosion-free environmentally friendly materials prolongs the service life of the equipment and reduces the waste generated by equipment replacement. The optimized mute and dust-proof design improves the production workshop environment, reduces noise and dust pollution, and creates a safer and more comfortable working space. Driven by the dual constraints of environmental protection policies and market demand, green upgrading has become the only way for the powder spraying machine industry. Future technological research and development will focus on low-carbon materials, ultra-low energy consumption operation and zero-emission recycling system, helping more manufacturing enterprises realize green transformation and contribute to the global goal of carbon peak and carbon neutrality.  
    LEER MÁS
  • Intelligent Empowerment of Powder Spraying Machines: Leading the Intelligent Reform of Coating Industry
    Intelligent Empowerment of Powder Spraying Machines: Leading the Intelligent Reform of Coating Industry
    May 12, 2026
    In the wave of Industry 4.0, intelligentization has become the core breakthrough point for the iterative upgrading of industrial equipment, and powder spraying machines are taking the lead in completing the transformation from traditional mechanical equipment to intelligent integrated equipment. It is no longer a simple spraying tool, but a smart terminal integrating perception, analysis, adjustment and execution, rewriting the operation mode of the entire coating industry.   Traditional powder spraying machines rely heavily on manual experience for parameter setting and operation adjustment. Workers need to repeatedly debug according to the shape, material and spraying requirements of workpieces, which not only has high technical threshold, but also easily causes unstable coating quality and inconsistent production standards. With the deep integration of IoT technology, AI algorithm and machine vision, modern powder spraying machines have broken this bottleneck thoroughly.   Machine vision recognition technology endows the spraying machine with "perception ability". It can automatically identify the contour, corner and special structure of irregular workpieces, independently plan the optimal spraying path, and avoid spraying dead angles and powder accumulation. No matter complex hardware parts, automotive accessories or household appliance shells, it can realize adaptive spraying without manual repeated programming.   The embedded intelligent algorithm realizes real-time dynamic optimization of spraying parameters. The equipment can monitor environmental temperature, humidity, powder flow and electrostatic voltage in real time, automatically adjust atomization volume and spraying distance according to changes in the production environment, and always maintain the best coating state. Meanwhile, the cloud interconnection function supports remote monitoring, data synchronization and fault early warning. Enterprises can view production data anytime and anywhere, realize predictive maintenance of equipment, and greatly reduce downtime losses.   Intelligent upgrading also brings qualitative changes to production management. The intelligent powder spraying production line can realize seamless connection with automated manipulators and assembly lines, forming an unmanned full-process operation mode from feeding, pretreatment, spraying to curing. It not only liberates labor, reduces human error interference, but also realizes standardized and streamlined production.   In the future, the intelligent evolution of powder spraying machines will continue to deepen. With the empowerment of digital twin technology and big data analysis, equipment will have stronger self-learning and process optimization capabilities, provide customized spraying solutions for different industries, and become an important cornerstone for manufacturing enterprises to build smart factories.
    LEER MÁS
  • How should small and medium-sized enterprises select appropriate spray painting equipment? Don't overlook these 4 key points
    Apr 13, 2026
    For small and medium-sized enterprises and individual operators, choosing a suitable spraying equipment can not only improve production efficiency and reduce costs, but also ensure product quality and enhance market competitiveness. But there are many types of spraying equipment on the market, including large automated production lines and portable spraying machines, and many companies do not know how to choose. Today, based on the characteristics of small and medium-sized enterprises, we will share four key points for selection to help everyone avoid pitfalls and choose the right equipment. Key point one: Choose equipment types based on production scale and demand. If the enterprise produces in small batches and multiple categories, such as small metal crafts, automotive repair parts, etc., it is recommended to choose a portable spray coating machine. The portable spray coating machine is compact, easy to carry, easy to operate, does not require a dedicated site, has low investment cost, and can flexibly adapt to the spraying needs of different scenarios; If the enterprise is engaged in large-scale and standardized production, such as household appliance casings, automotive parts, etc., it is recommended to choose an automated spray coating production line. Although the initial investment is high, the production efficiency is high, the coating quality is stable, and long-term use is more cost-effective. Key point two: Pay attention to the core performance and stability of the device. Regardless of which device is chosen, core performance is crucial. For spray painting machines, attention should be paid to the atomization effect of the spray gun, the range of powder output adjustment, and the stability of electrostatic voltage, which directly affect the quality of the coating; The stability of the powder supply device is also important to ensure uniform and continuous powder feeding, and to avoid powder breakage; The curing oven should be able to accurately control temperature to ensure that the coating is fully cured. It is recommended to choose brands with good reputation and guaranteed quality, and avoid purchasing cheap equipment, which may result in high maintenance costs and affect production in the later stage. Key point three: Consider environmental and cost factors. Under the "paint to powder" policy, environmental compliance is the bottom line for enterprises. The selected spraying equipment should meet environmental requirements, preferably equipped with a powder recycling system to improve powder utilization, reduce waste and environmental pollution. At the same time, the energy consumption and maintenance costs of the equipment should be considered. Portable spray painting machines have low energy consumption and simple maintenance, making them suitable for small and medium-sized enterprises; Automated production lines have high energy consumption, but unit costs can be reduced through large-scale production. Key point four: Choose based on one's own technical level. Small and medium-sized enterprises often lack professional spray coating technicians, so the equipment selection threshold should not be too high. It is best to have simple and easy to operate equipment, and the manufacturer can provide comprehensive technical training and after-sales service. For example, portable spray painting machines can be operated by ordinary workers after simple training, and manufacturers provide on-site maintenance services, which can reduce the technical pressure and maintenance costs of enterprises. To sum up, small and medium-sized enterprises should follow the principle of "choosing according to needs, focusing on performance, taking into account environmental protection, and being suitable for themselves" when choosing spray painting equipment. They should not blindly pursue high-end equipment, nor be tempted by cheapness. What suits them is the best.
    LEER MÁS
  • Common Faults and Solutions in Powder Coating: This Guide Will Last You a Year
    Apr 13, 2026
    In the process of powder coating, many enterprises will encounter various faults, such as coating peeling, bubbles, sagging, color difference, etc., which not only affect product quality, but also reduce production efficiency and increase costs. I have been working in the powder coating industry for many years, and I have compiled the 6 most common faults and detailed solutions. I have collected this article so that you don't have to panic when encountering problems in the future. Fault 1: Coating peeling and poor adhesion. There are three main reasons: firstly, incomplete pre-treatment of the workpiece, resulting in oil stains, rust, and dust on the surface; Secondly, the curing temperature or time is insufficient, resulting in insufficient curing of the coating; The third issue is the poor quality of powder coating, which does not match the material of the workpiece. Solution: Thoroughly clean the surface of the workpiece, remove impurities through grinding, acid washing, and other methods to ensure a dry and smooth surface; Strictly adjust the curing temperature and time according to the powder instructions to ensure that the coating is fully cured; Choose high-quality powder coating that matches the material of the workpiece. Fault 2: There are bubbles and pinholes in the coating. Main reasons: There is moisture and oil on the surface of the workpiece, and bubbles are generated when the moisture evaporates during spraying; Powder coating becomes damp and clumps, resulting in pinholes after spraying; There are impurities in the curing oven that adhere to the surface of the coating. Solution: After pre-processing, the workpiece should be thoroughly dried to avoid surface moisture; When storing powder coatings, keep them dry. After being damp, they can be dried before use; Regularly clean the curing furnace to keep it clean. Fault 3: Coating sagging and uneven thickness. Main reasons: The distance between the spray gun and the workpiece is too close, and the dwell time is too long; Excessive powder output and high electrostatic voltage; Uneven movement speed during spraying. Solution: Adjust the distance between the spray gun and the workpiece (15-25cm), move the spray gun at a constant speed to avoid stopping; Adjust the powder output and electrostatic voltage according to the workpiece requirements to avoid excessive powder output; Strengthen operator training and standardize operating procedures. Fault 4: Obvious color difference in coating. Main reason: Different batches of powder coatings result in color differences; Inconsistent spraying parameters and varying coating thicknesses; Uneven curing temperature leads to color changes. Solution: Try to use the same batch of powder coating as much as possible, and conduct small batch trial spraying for different batches first; Unified spraying parameters to ensure uniform coating thickness; Check the temperature of the curing furnace to ensure uniform temperature inside the furnace. Fault 5: The powder does not apply and the adsorption effect is poor. Main reasons: Low static voltage, insufficient powder charging; The workpiece is not grounded or poorly grounded; Poor flowability of powder coating and blockage of spray gun due to clumping. Solution: Increase the electrostatic voltage to ensure that the powder is fully charged; Check the grounding condition of the workpiece to ensure good grounding; Clean the spray gun and powder supply device, crush the agglomerated powder, and ensure the flowability of the powder. Fault 6: There are impurities and particles on the surface of the coating. Main reason: There is dust in the spraying environment, which adheres to the surface of the workpiece; Impurities are present in powder coatings; There are debris inside the spray gun, blocking the powder outlet. Solution: Keep the spraying environment clean and clean it regularly; Filter the powder coating before use to remove impurities; Regularly clean the spray gun and keep the powder outlet unobstructed.
    LEER MÁS
  • 2026 Powder Coating Industry Trend Forecast: These Three Directions Merit Special Attention
    Apr 13, 2026
    With the continuous tightening of environmental policies, the rapid advancement of intelligent manufacturing, and the rise of emerging industries, the powder coating industry is facing unprecedented development opportunities. As an industry practitioner, combined with the latest industry reports and market trends, today we will talk about the three major development trends of the powder coating industry in 2026, hoping to provide reference for everyone's enterprise development and personal career planning. Trend 1: Environmental protection continues to upgrade, and low-carbon has become the core competitiveness of the industry. With the advancement of the "dual carbon" target and the continuous tightening of environmental policies, low VOC and VOC free powder coatings will become the mainstream in the market. It is expected that the market share of low VOC powder coatings will further increase to over 50% by 2026. At the same time, the low-carbon value chain of powder coating will become a key focus. Enterprises will start from the entire process of raw material selection, production technology, and recycling system to reduce carbon emissions. The cooperation between giants such as BASF and AkzoNobel is a good example. In addition, the dividends of environmental policies will continue to be released, and the "double tax exemption" policy will further promote the process of "paint to powder". Environmental compliance will become the bottom line for the survival of enterprises. Trend 2: Intelligent and automated accelerated penetration, unmanned spraying has become a new hotspot. With the advancement of Industry 4.0, intelligent spraying technology will gradually become popular. Machine vision, big data, artificial intelligence and other technologies will be deeply integrated with powder spraying equipment to achieve real-time monitoring, parameter optimization and defect warning of the spraying process. The application of unmanned spraying lines will become increasingly widespread, reducing manual intervention, lowering labor costs and production risks. It is expected that by 2026, the penetration rate of automated powder spraying equipment will reach over 40%, and small enterprises will gradually introduce intelligent equipment to improve production efficiency and product quality. Trend 3: The application areas continue to expand, and emerging fields have become new growth points. The traditional fields of automobiles, home appliances, and building materials will continue to maintain stable growth, while emerging fields such as new energy vehicles, photovoltaics, rail transit, and medical equipment will become the core driving force for industry growth. For example, the demand for lightweight and highly corrosion-resistant powder coatings in new energy vehicles has surged, and high-performance powder coatings are also needed for surface protection of photovoltaic modules. The demand in these emerging fields will drive the innovation of powder coating technology and product upgrades. At the same time, the popularization of portable spray painting machines will further expand the subdivision scenarios such as on-site maintenance and small product processing, enriching the industry application scenarios. Opportunities and challenges coexist. In 2026, the powder coating industry will enter a stage of high-quality development. Only by keeping up with industry trends, increasing research and development investment, and enhancing core competitiveness can we stand out in industry competition.
    LEER MÁS
  • Powder coating vs traditional painting: After reading this article, you'll know how to make the right choice.
    Apr 04, 2026
    In the field of industrial surface treatment, powder coating and traditional spray painting are the two most common coating methods, and many companies are hesitant when choosing: which one is more suitable for themselves? Today, we will make a detailed comparison in terms of environmental protection, cost, effectiveness, and applicable scenarios to help everyone make the best choice. From an environmental perspective, powder coating is superior to traditional spray painting. Traditional spray painting uses organic solvents, which generate a large amount of VOCs emissions and pollute the environment. It also requires a significant investment in the construction of end of pipe treatment facilities, otherwise it cannot meet environmental standards; Powder coating has no VOCs emissions, and the overspray powder can be recycled and reused with a utilization rate of over 95%. It not only complies with national environmental protection policies, but also reduces environmental pollution. It is currently one of the most environmentally friendly coating methods, especially suitable for enterprise transformation under the "paint to powder" policy. From a cost perspective, powder coating has more advantages over long-term use. The utilization rate of traditional spray paint coatings is only 30% -50%, resulting in a large amount of paint waste, high prices of organic solvents, and high environmental management costs; Although the initial equipment investment for powder spraying may be slightly higher, the powder utilization rate is high, there is no solvent consumption, and the cost of environmental protection is low. Long term use can significantly reduce coating costs. For small and micro enterprises engaged in small-scale production, the emergence of portable spray painting machines has further lowered the entry threshold for powder spraying, resulting in higher cost-effectiveness. From the perspective of coating effect, powder coating is more durable and uniform. The adhesion, hardness, corrosion resistance, and weather resistance of powder coating are superior to traditional spray painting. The coating thickness is uniform and not prone to defects such as sagging, bubbles, and peeling, providing long-term protection for workpieces; Traditional spray paint coatings are thinner, have poor anti-corrosion performance, are prone to fading, paint peeling and other problems, and have a shorter service life. From the perspective of applicable scenarios, both have their own focuses. Powder coating is suitable for metal workpieces, such as automotive parts, home appliance casings, metal furniture, building materials, etc., especially for scenarios with high requirements for corrosion resistance and wear resistance; Traditional spray painting is suitable for non-metallic workpieces such as plastic, wood, etc., and is also suitable for scenes that require high painting accuracy and multiple color gradients. To sum up, if your company focuses on metal workpieces, pays attention to environmental protection, cost, and coating durability, especially under the "paint to powder" policy, powder coating is definitely the first choice; If it is a non-metallic workpiece with high requirements for coating accuracy and color diversity, traditional spray painting can be chosen.
    LEER MÁS
  • Essential Guide for Beginners: Operational Manual for Portable Spray Painting Machines to Avoid Common Pitfalls and Minimize Missteps
    Apr 04, 2026
    As a veteran who has been working in the industrial coating industry for 8 years, I am often asked by novice friends, "How to operate a portable spray coating machine? Why does the coating I spray always have unevenness and bubbles?" In fact, the operation of a portable spray coating machine is not difficult, but many beginners are prone to some misunderstandings, which can lead to poor coating effects. Today, I will compile a detailed operation guide to help you avoid misunderstandings and quickly get started. Firstly, sufficient preparation work must be done before operation. Many beginners are eager to start work and neglect the pre-treatment of workpieces, which is the main reason for coating peeling and bubbles. The surface of the workpiece must be cleaned thoroughly to remove impurities such as oil, rust, dust, etc. It can be treated by grinding, acid washing, phosphating, etc. to ensure that the surface is dry and flat. At the same time, it is necessary to check the spraying machine equipment to confirm that the spray gun, powder supply device, air compressor, etc. are operating normally, and that the powder coating is not clumped or deteriorated. Secondly, master the correct spraying techniques. When spraying, it is recommended to maintain a distance of 15-25cm between the spray gun and the workpiece, control the angle between 45 ° -90 °, and move at a constant speed to avoid staying for too long and causing the coating to become too thick or hang. The powder output and electrostatic voltage should be adjusted according to the material of the workpiece and the type of powder. Generally speaking, the electrostatic voltage can be appropriately increased for metal workpieces, and the powder output can be reduced when the powder particles are finer. In addition, the spraying environment is also important. It is recommended to operate in a ventilated, dry, and dust-free environment, with a temperature control of 15-30 ℃ and humidity not exceeding 70%, to avoid dust adhering to the surface of the workpiece. Then, the high-temperature curing process cannot be taken lightly. Different types of powder coatings have different curing temperatures and times, generally ranging from 160-220 ℃ and curing times of 15-30 minutes. It is important to strictly follow the powder instructions and not lower the temperature or shorten the time arbitrarily, otherwise it will result in insufficient coating curing, insufficient hardness, and easy detachment. After curing, the workpiece should be allowed to cool naturally to avoid immediate contact with cold water and prevent coating cracking. Finally, share a few common misconceptions. One is that it is believed that "the more powder is produced, the thicker the coating, the better". However, excessive coating thickness can lead to sagging, bubbles, and affect aesthetics and adhesion; Secondly, neglecting powder recycling not only wastes raw materials but also pollutes the environment; Thirdly, long-term failure to clean the spray gun and powder supply device leads to powder blockage, which affects the spraying effect. As long as you avoid these misconceptions and strictly follow the operating instructions, even beginners can spray a uniform, beautiful, and durable coating.
    LEER MÁS
1 2 3

dejar un mensaje

dejar un mensaje
Si está interesado en nuestros productos y desea conocer más detalles, deje un mensaje aquí, le responderemos lo antes posible.
entregar

Nuestro horario

Lunes - Sábado: 8:00 a. m. - 6:00 p. m.

CONTÁCTENOS :lvobo2026@gmail.com

Hogar

Productos

whatsApp

contacto